Ramp up electronics production
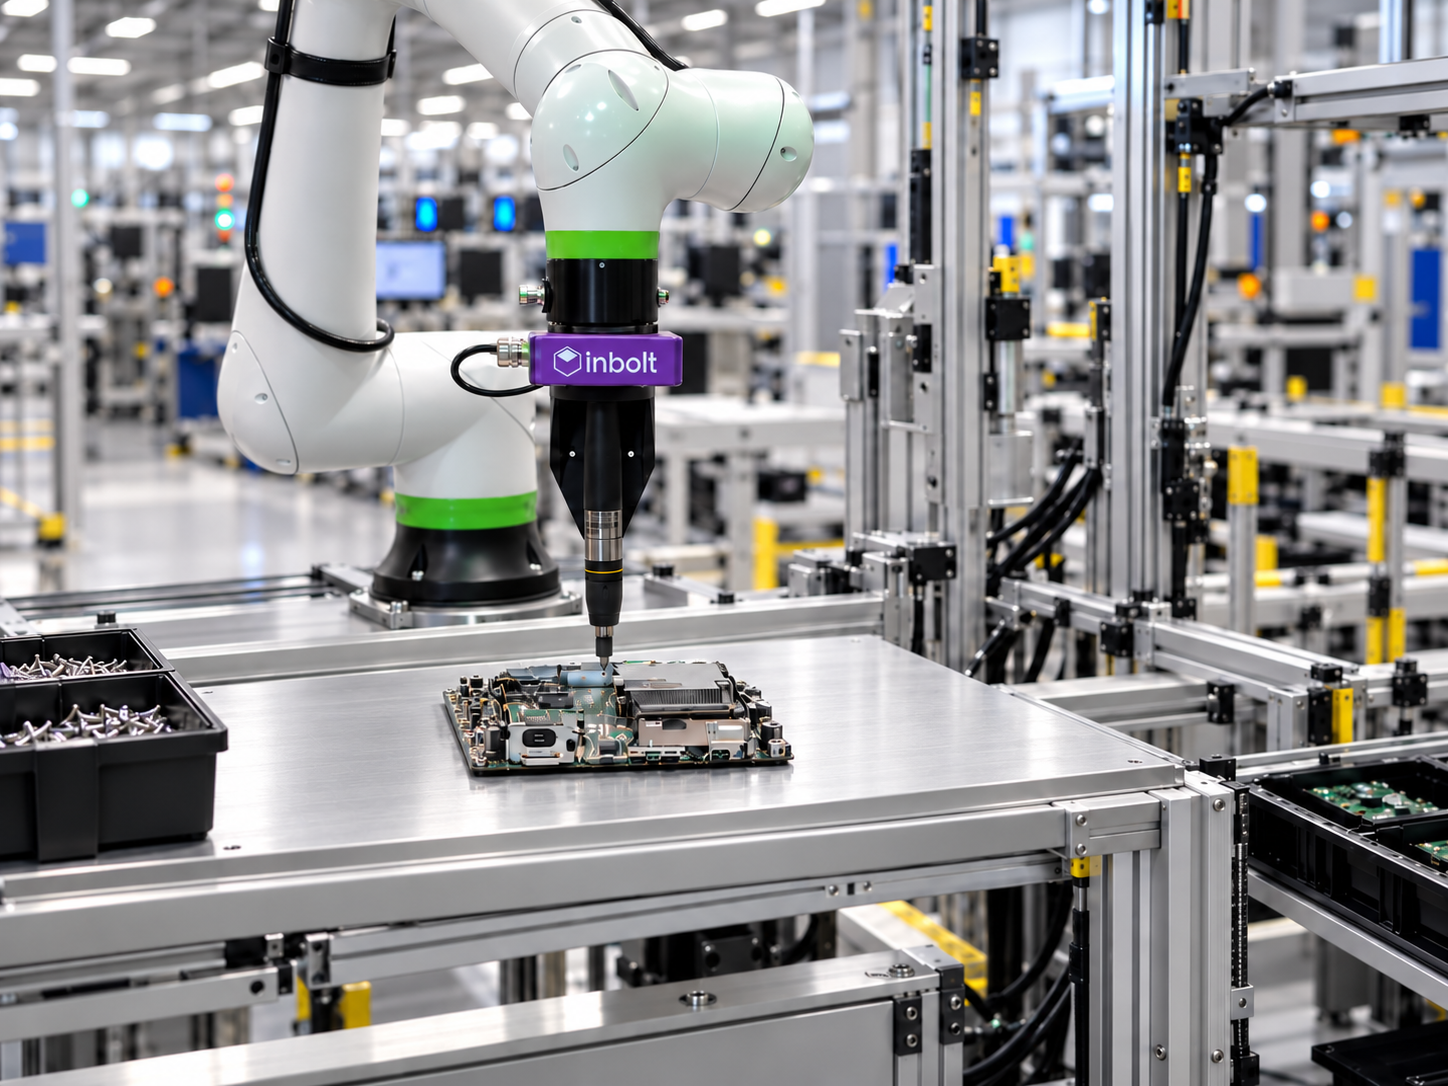
Program your robots offline from CAD, and Inbolt’s vision model corrects every path to where the part actually sits on the line. Each new product goes from design to volume without building fixtures or re-teaching robots on the floor.
The embedded brain of your assembly line
One vision system that mounts to the robot, learns from CAD and stays inside your plant.

One controller, one camera, no fixtures
Inbolt mounts to the robot and trains from your CAD model directly. No jigs, no mechanical indexing, no six-figure fixture package per station.

Runs on the robot you already have
Native to FANUC, ABB, KUKA, Yaskawa, Universal Robots and Comau. Approve it once, deploy it across every plant running a mixed fleet.

Everything stays on your network
Training and inference run entirely on premise. No cloud, no dataset upload, no vendor in the loop for routine part changes.
Proven impact, measurable results
5
< 5 min
CAD training time
0.5
< 0.5 mm
Localization accuracy
200
200 +
Systems in production
40
40 M
Robot cycles powered in 2025
Why robot deployment slows every product launch
Every new product means new robot programs, and today that work happens on the line: engineers teach points by hand, then re-teach after every design revision. Offline programming should remove that work, but a simulated program assumes the part sits exactly where the CAD says, so it needs a fixture to hold it there.
A fixture is a mechanical answer to an information problem. That works when a part lasts for years. It fails when a server generation lasts 12 to 18 months, and each one changes geometry, fasteners and connector positions. Every revision means new fixtures to design, build and validate, and new weeks of commissioning.
Inbolt inverts that. The program exists as soon as the CAD does, and vision corrects it to the real part every cycle. New variant, new CAD file, not new fixtures. For NPI teams judged on time from design freeze to a qualified line, that’s the difference between a first batch that ships and one that’s scrapped.
How it works
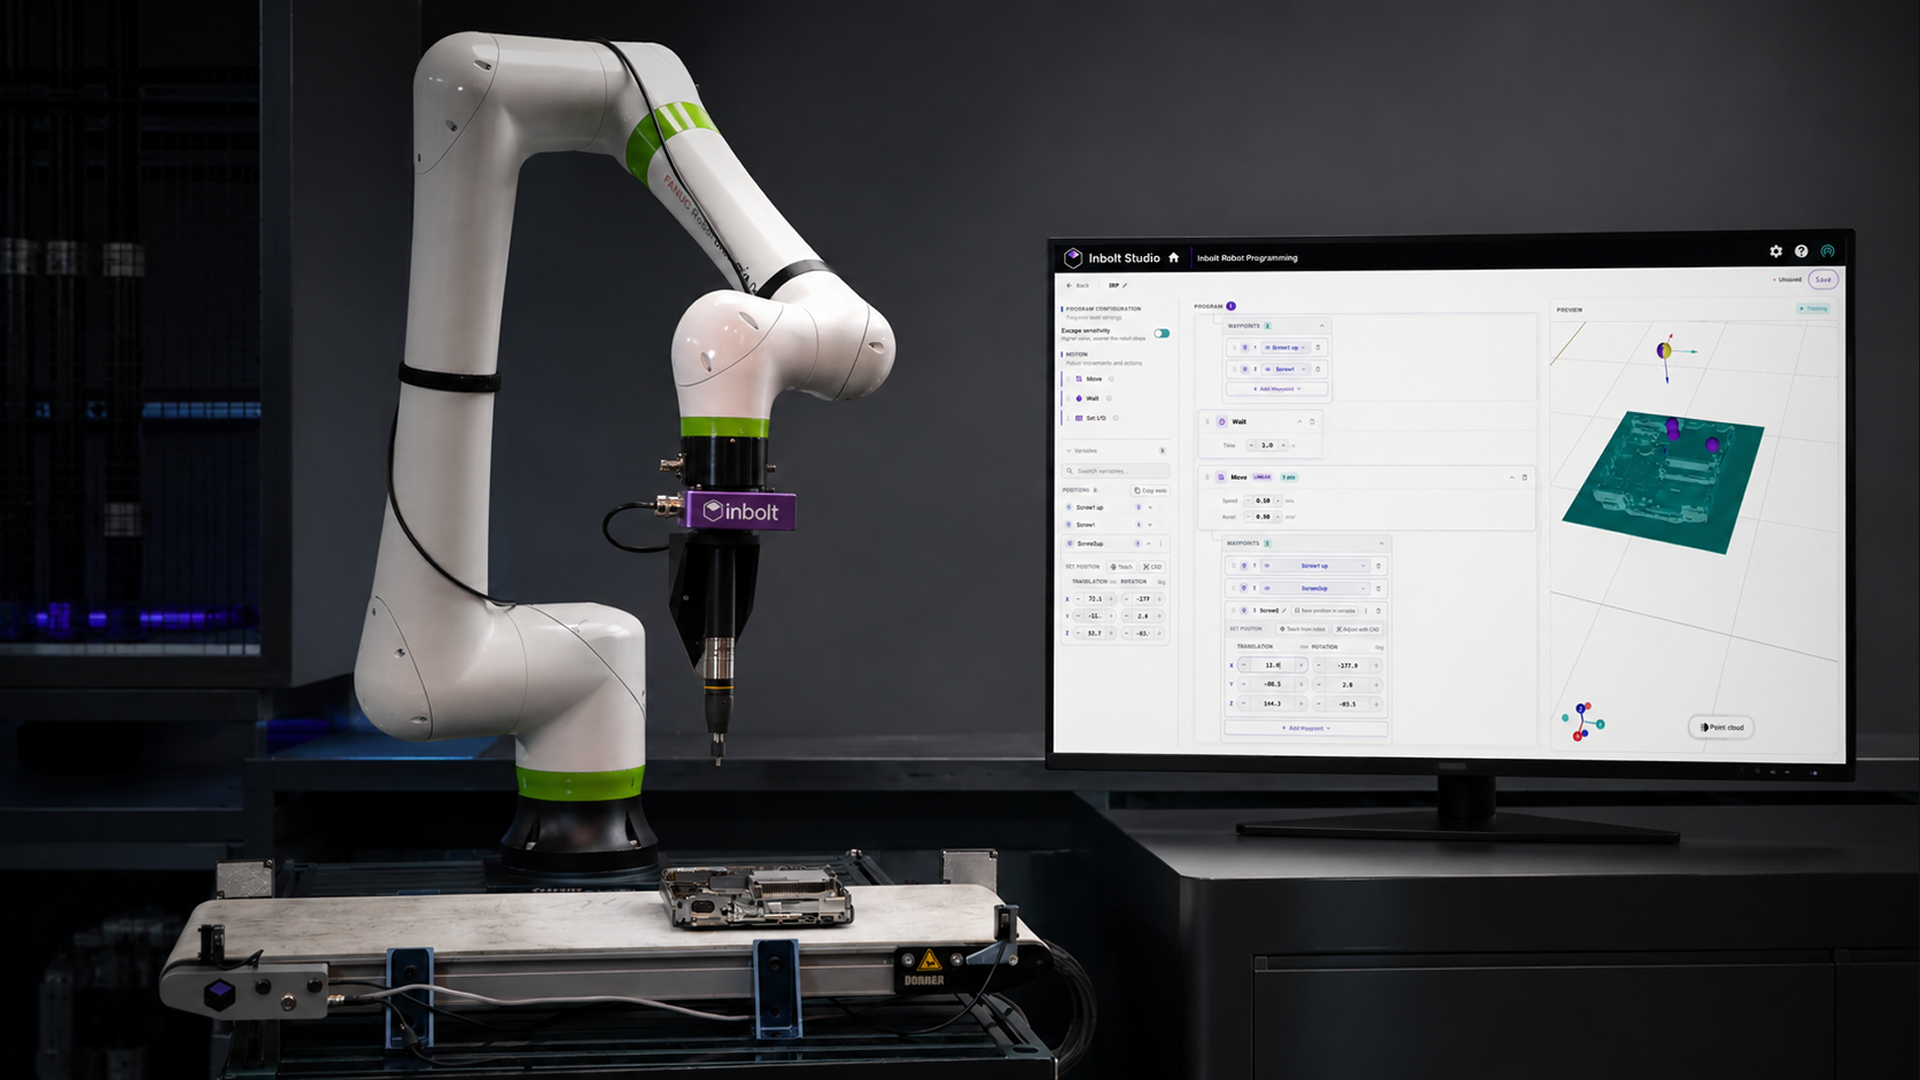
From CAD file to a running station in under a day.
Step 1 – Program offline
Generate the robot program from the CAD model in Inbolt Robot Programming, in minutes and away from the line.
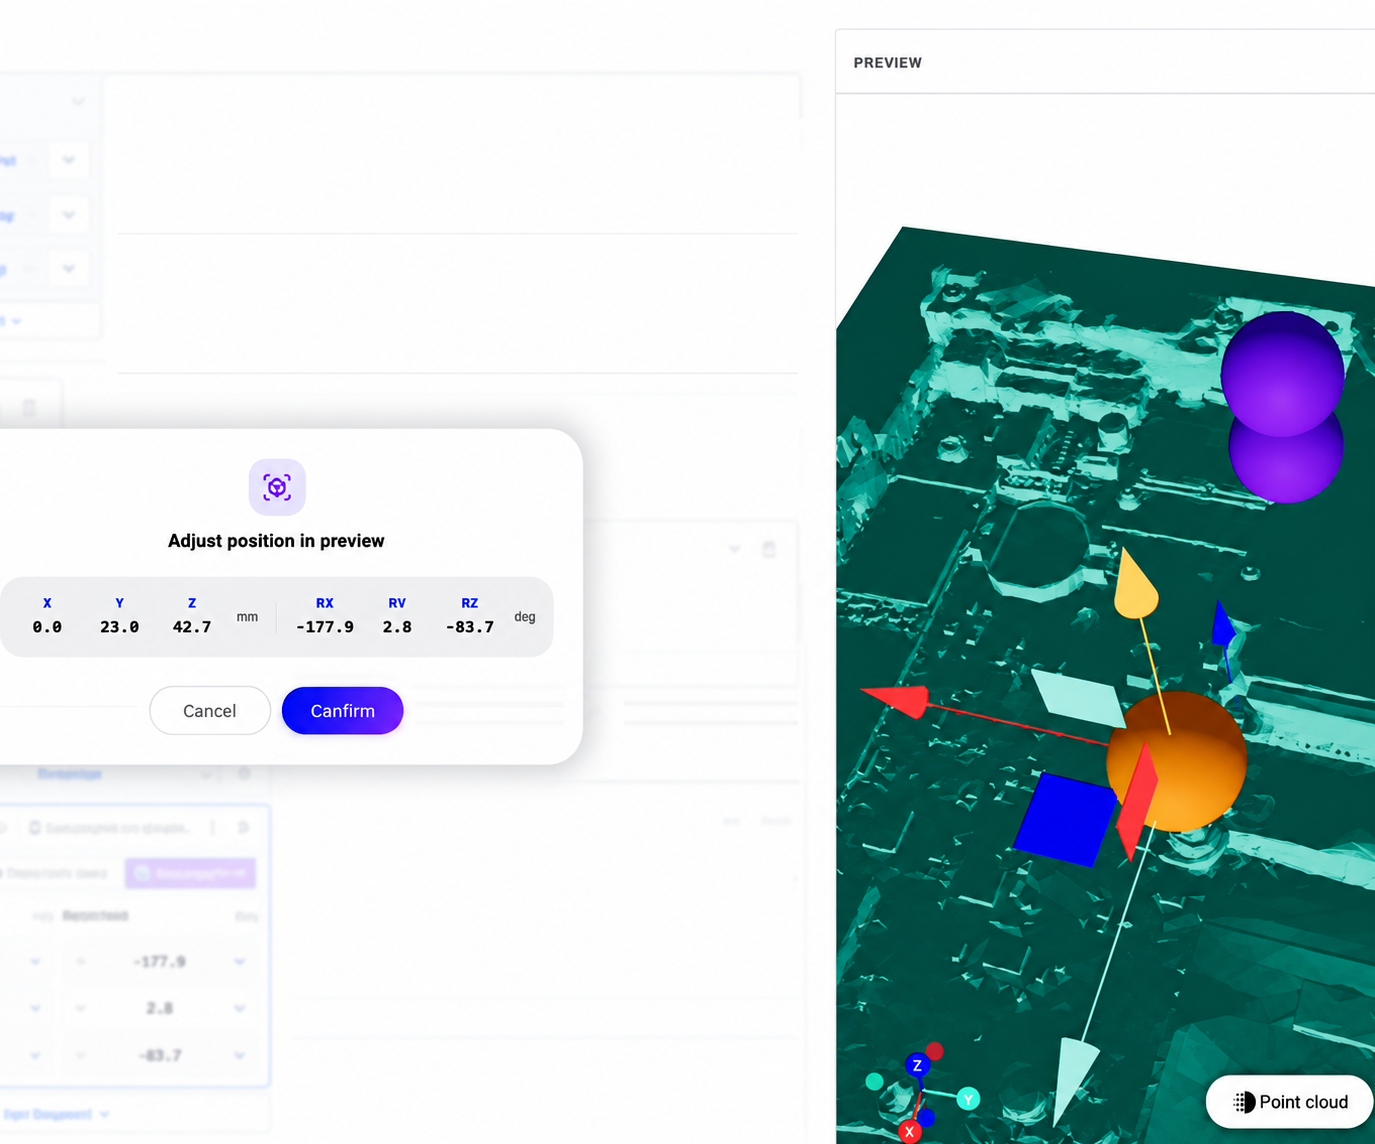
Step 2 – Train from CAD
Train vision on site in under five minutes, with the CAD file as the only input. No datasets, no labelling, no images to collect, and no cloud access required.
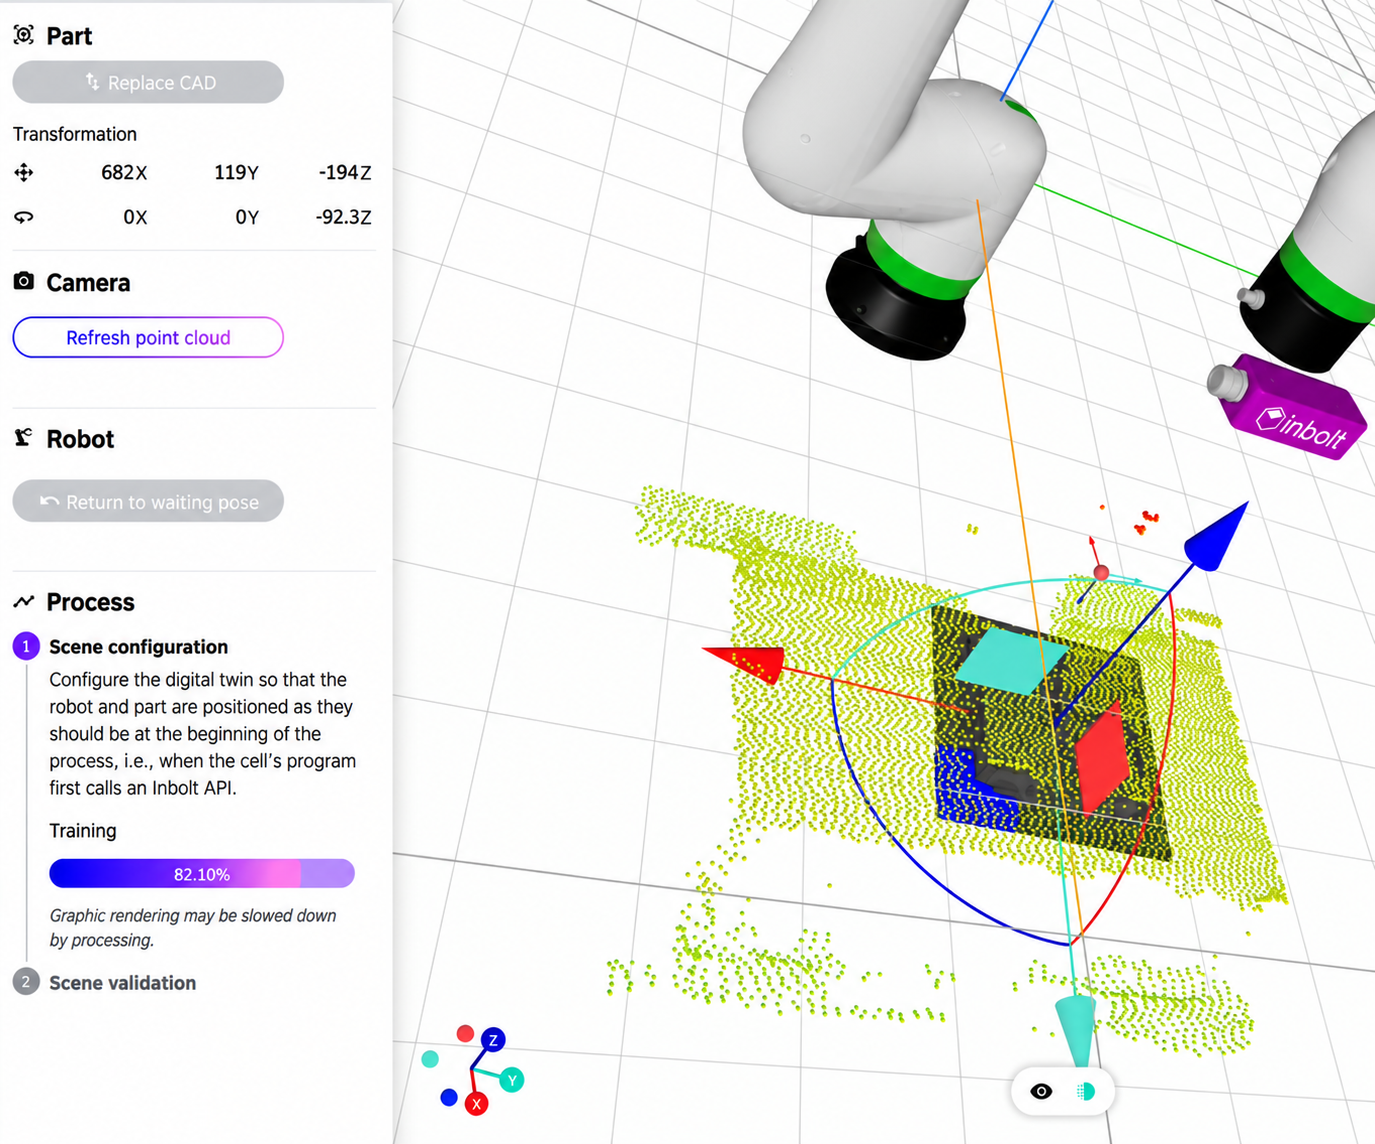
Step 3 – Run
The robot locates the real part and corrects its path in real time, every cycle, on the part as it actually sits.
What Inbolt adds to your line
One vision system across fastening, assembly, handling and tending.
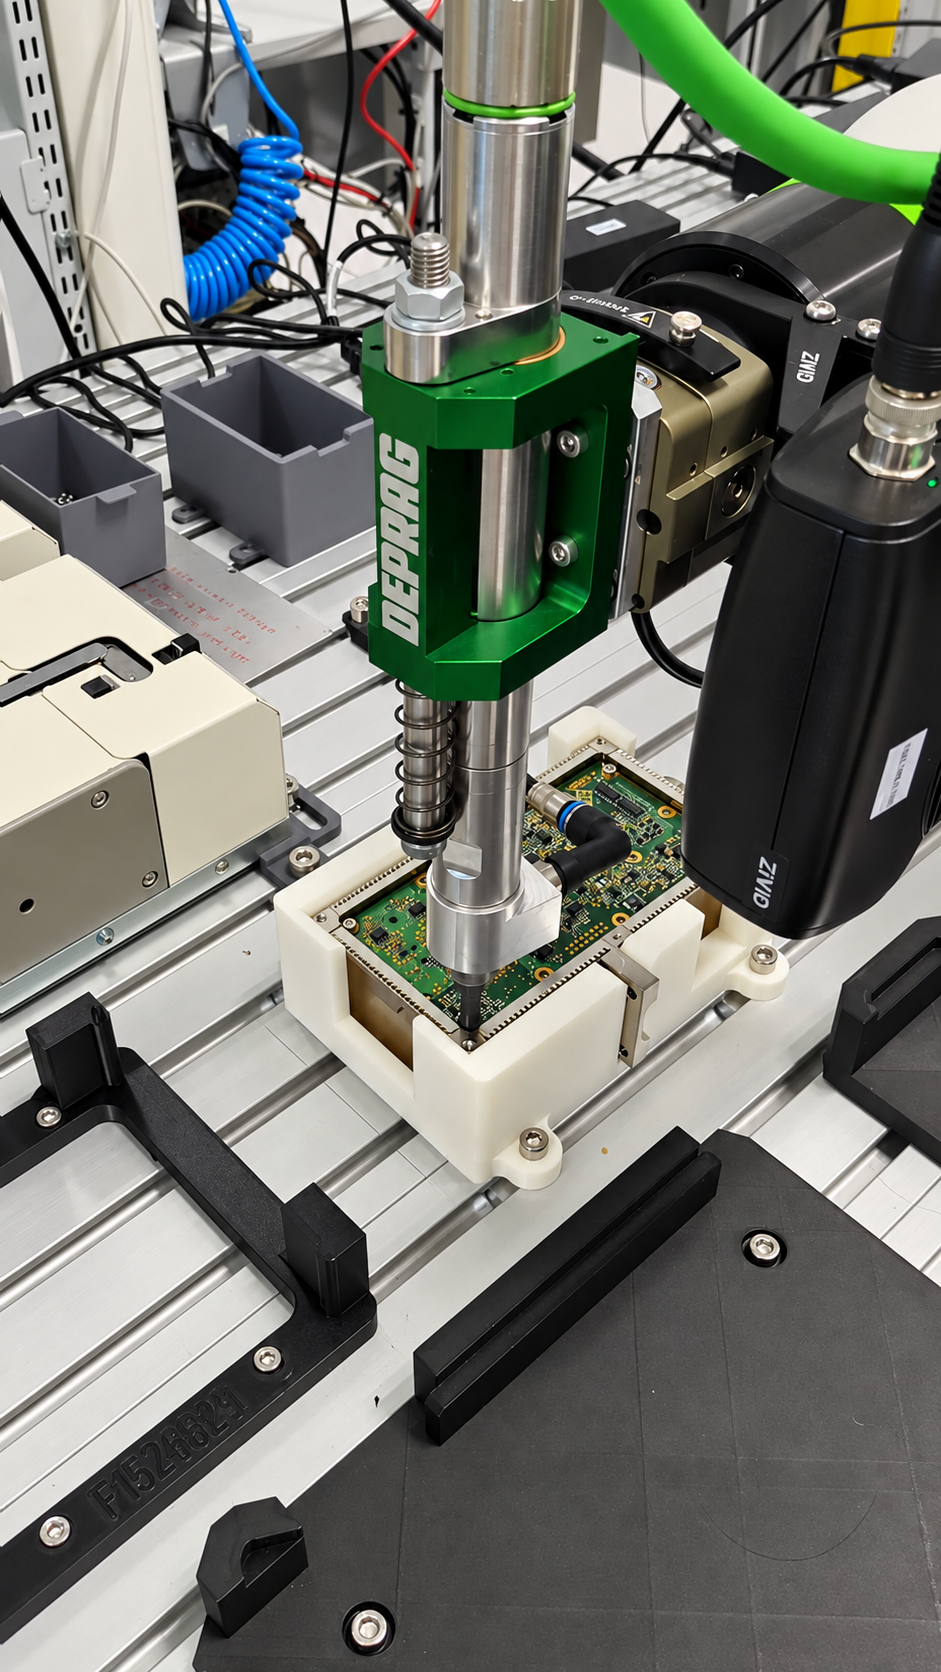
Fastening & torquing
Riveting
Module & card insertion
Component placement
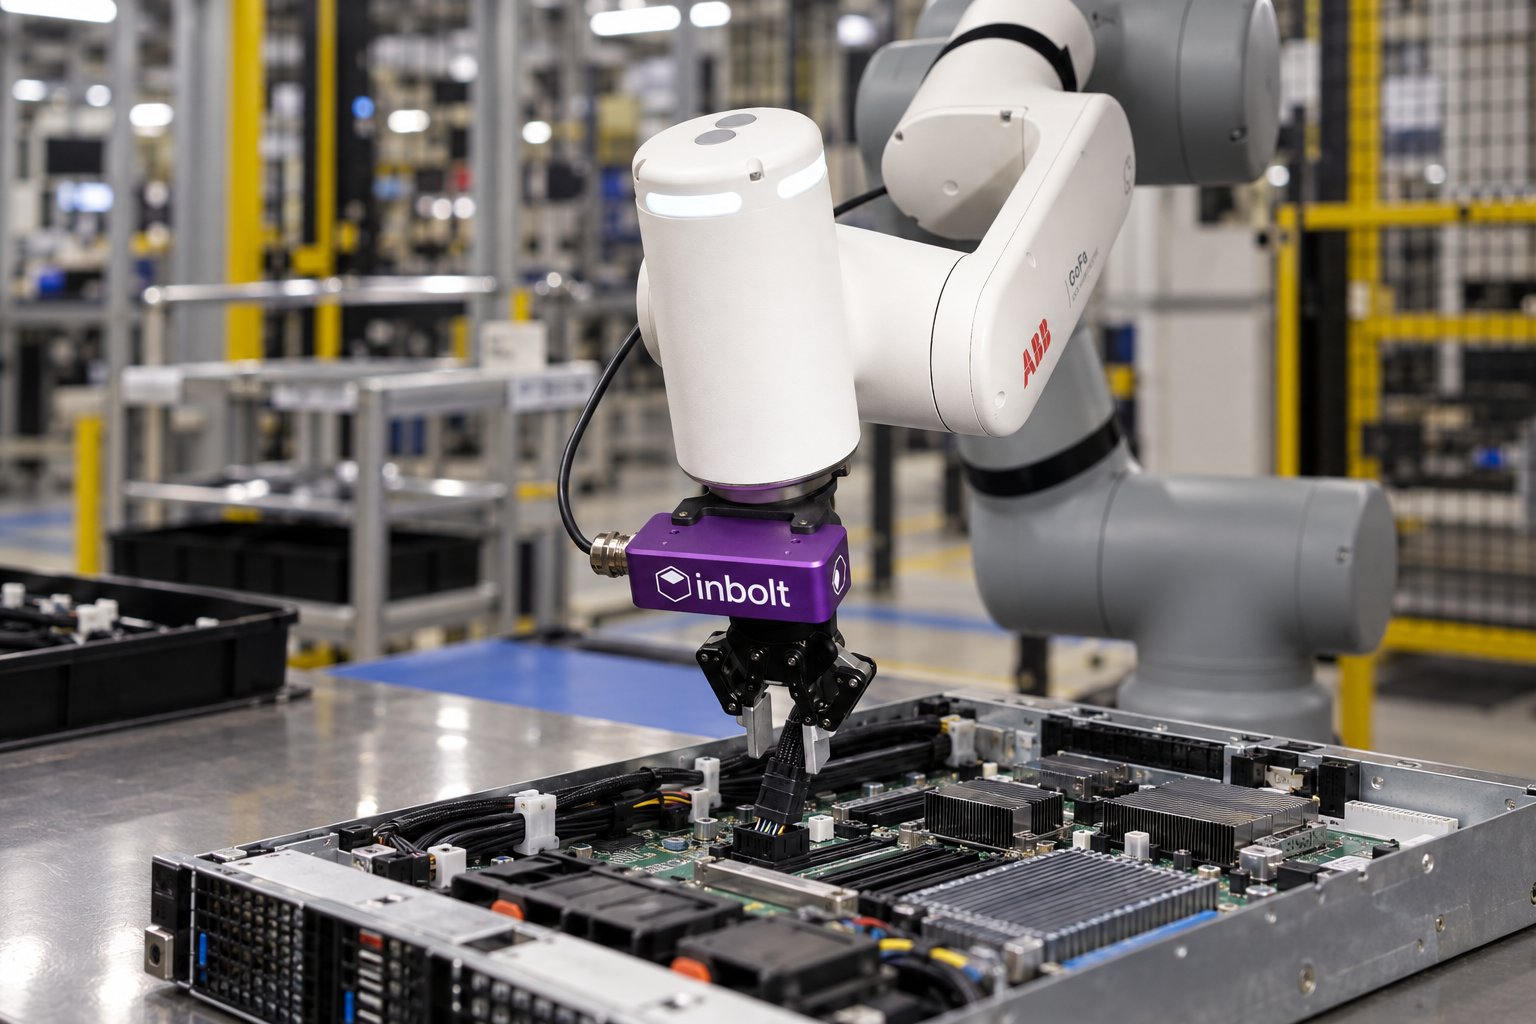
Cable & harness routing
Dispensing & sealing
Material handling
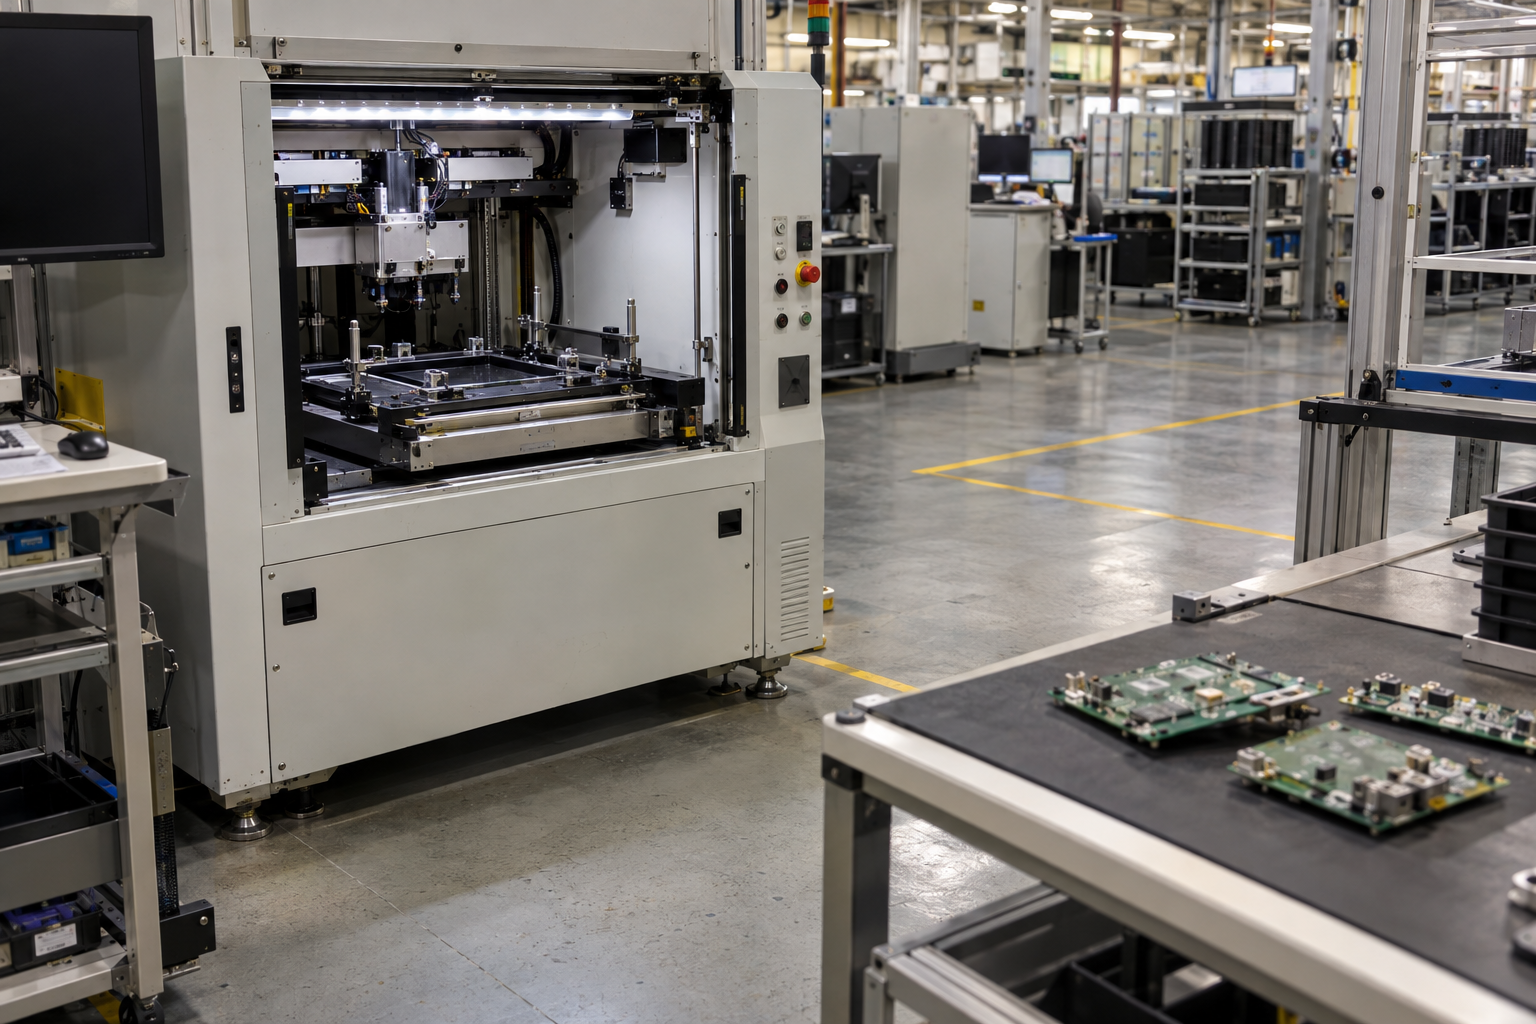
Machine tending

FAQ
Answers to common questions about Inbolt’s electronics manufacturing solution.

-
Ask what actually failed — usually it’s the hardware surviving the environment, or a dependency on the vendor for every change. Inbolt trains on your own machine, on premise, in about five minutes, and generates Python your engineers can read and change.
-
Yes, on parts down to roughly 1 cm, guided to sub-millimetre precision. Below that — PCB placement, die attach, wafer handling — you’re in placement-machine territory, and we’ll tell you so.
-
No. Training and inference both run on premise. Nothing leaves your network unless you choose to give us remote access.
-
Yes, and that’s the common need in this industry.
-
Yes, without a support ticket. One controller can run around 50 part numbers on the same station.
-
Minutes, not weeks. Engineers build the robot program directly from the CAD model in Inbolt Studio, without a teach pendant and away from the line. Training the vision system on the same CAD takes under five minutes. On the line, Inbolt locates the real part and the robot runs the planned path, so the iterative commissioning that usually takes weeks happens in one pass.
-
Not needed. Programming and vision training can be done offline on the Inbolt Platform. Engineers build the program from CAD in the part’s own reference frame, and the vision model adapts it to where the part actually sits at runtime. That means there’s no simulation-to-reality gap to close with fixtures or manual re-teaching. Inbolt Robot Programming is available today for FANUC, Universal Robots and Yaskawa, with more brands to follow.
Bring your next program to volume without the fixture lead time.
Tell us what’s on your “cannot be automated” list. We’ll tell you honestly whether precision is the blocker.
Explore more from Inbolt
Access articles, use cases, and resources to see how Inbolt drives intelligent automation worldwide.
Inbolt Product Brochure
Inbolt named as the #3 fastest growing startup by Sifted